Featured Cabinet Profiles, Edge Pulls & Architectural Hardware
Explore precision-machined edge grips, concealed motion dampers, structural aluminum hanging units, and high-tolerance architectural hardware built to rigorous industrial standards.
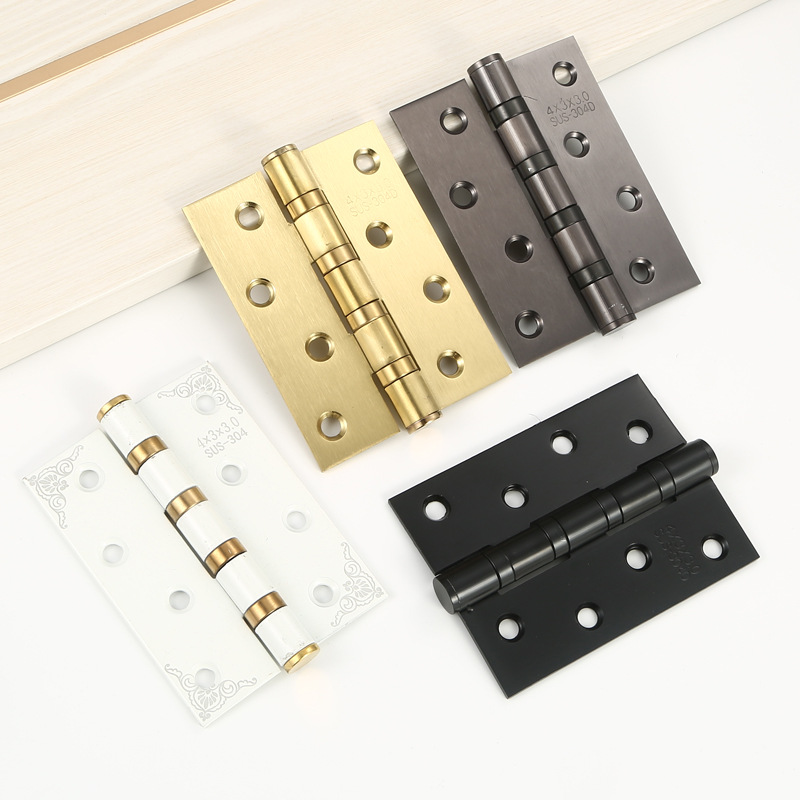
Solid forged brass pivot hinge engineered with an 8-hole template for heavy-duty flush cabinetry and commercial timber doors.
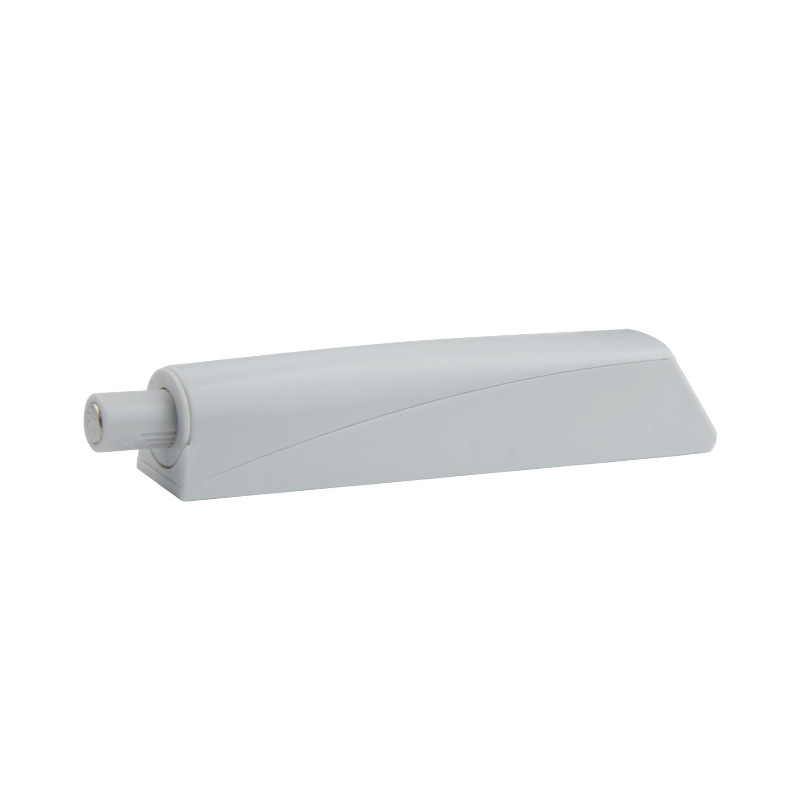
Integrated mechanical touch-latch mechanism enabling completely handle-free, seamless slab facades with adjustable magnetic rebound.
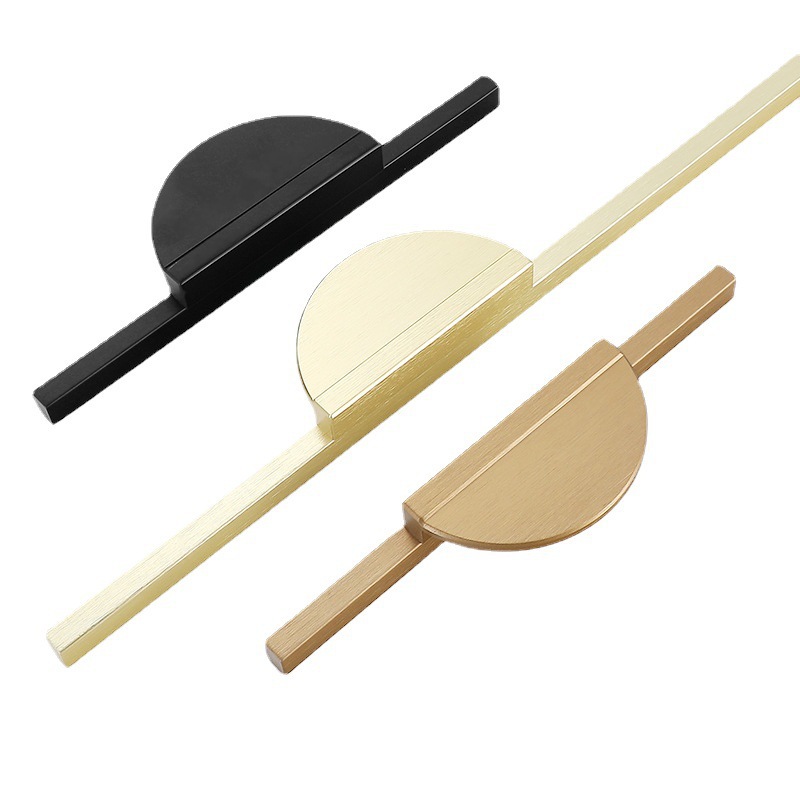
Modular paired edge design crafted from high-purity die-cast zinc alloy, offering geometric harmony on wardrobe and vanity drawers.
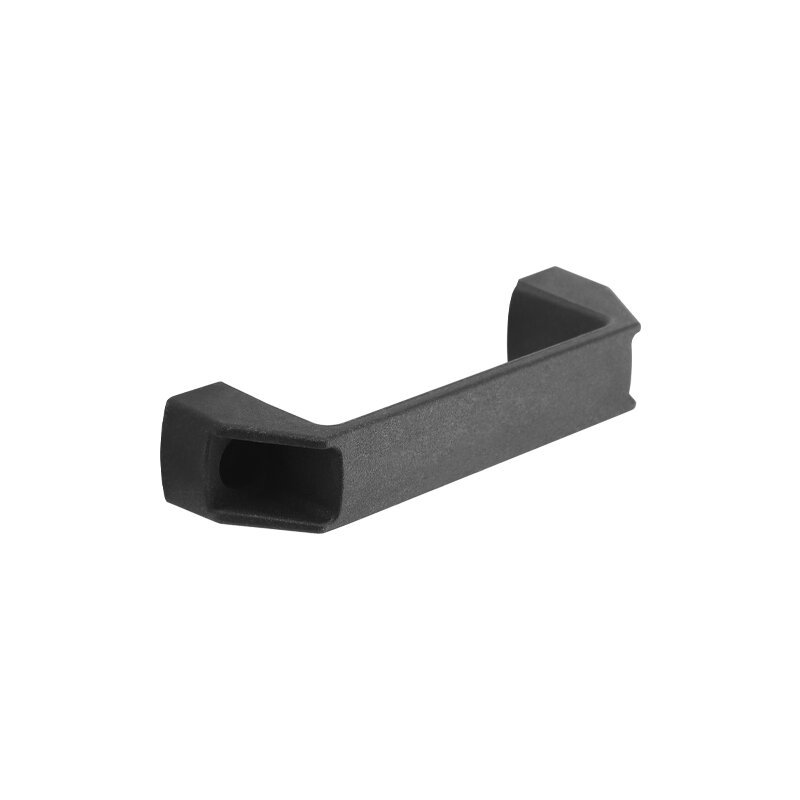
High-impact composite polymer grip handle engineered to withstand rigorous industrial environments, machinery enclosures, and workshops.
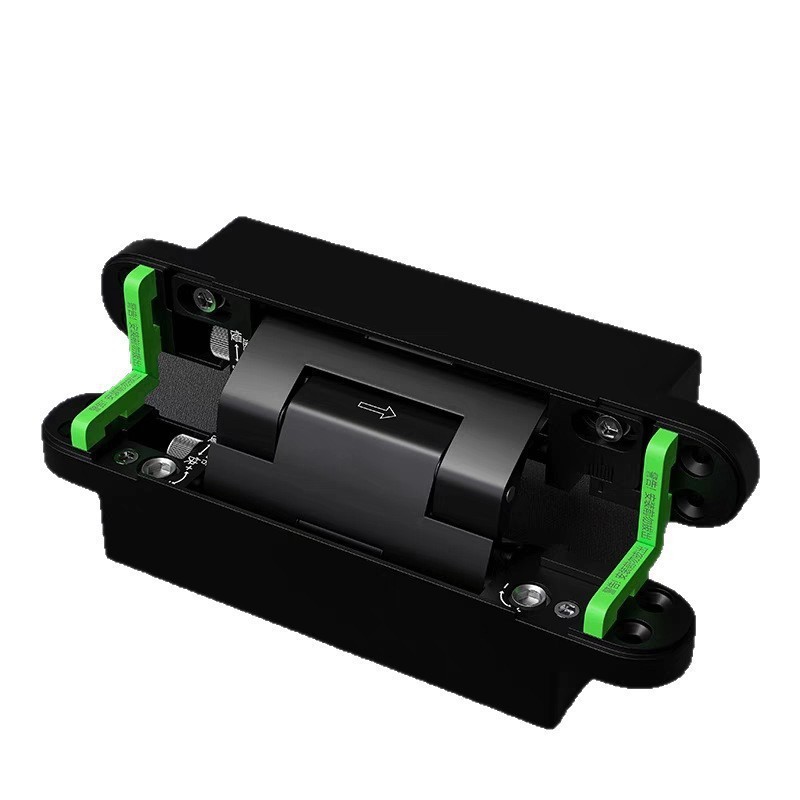
Completely invisible flush hinge featuring multi-axis 3D micro-adjustability for frameless doors and bespoke interior millwork.
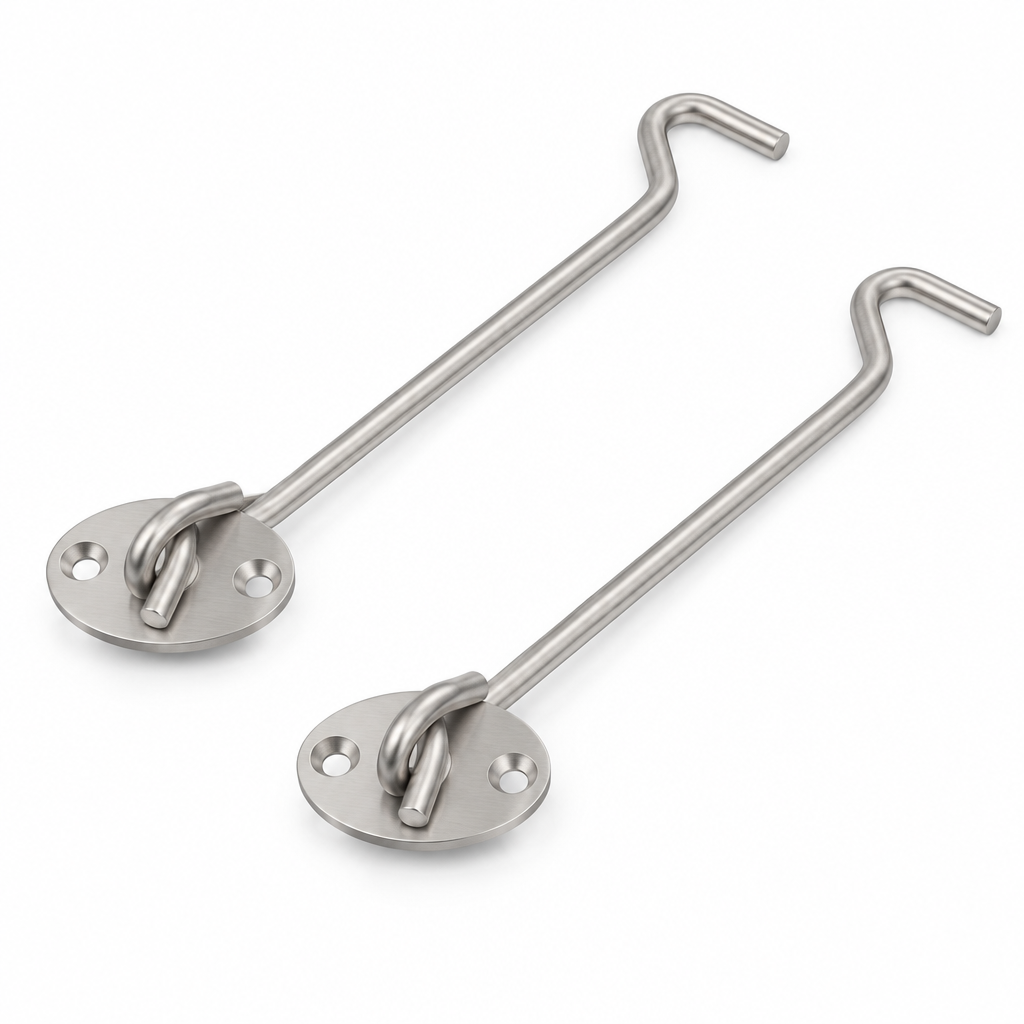
Grade 304 anti-corrosive security cabin hook and door stay hardware designed for moisture-exposed architectural doors and gates.
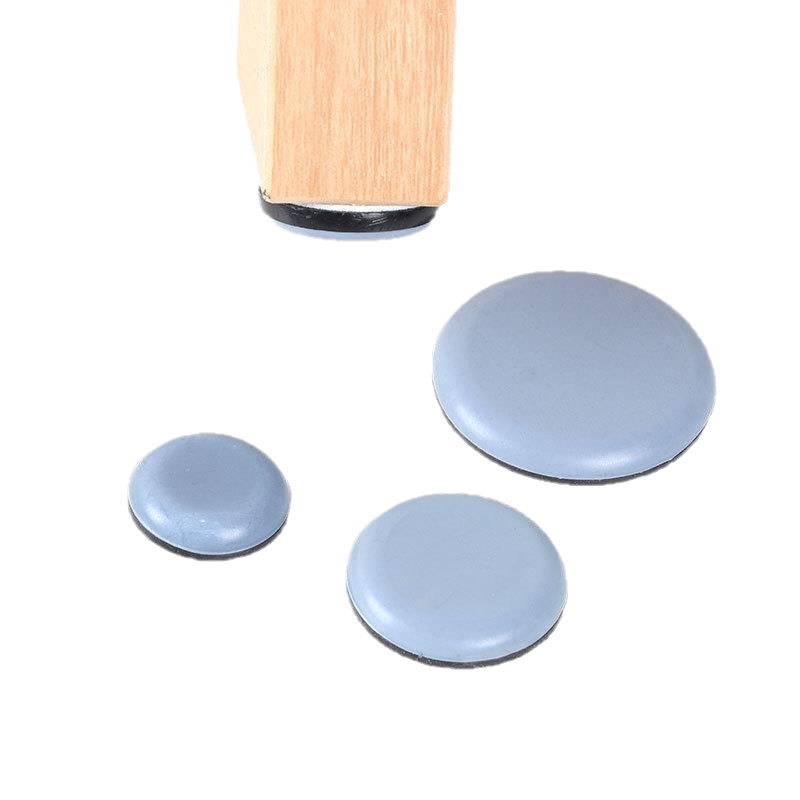
Ultra-low-friction fluoropolymer floor contact gliders with high-shear adhesive backings for commercial fit-outs and residential cabinetry.
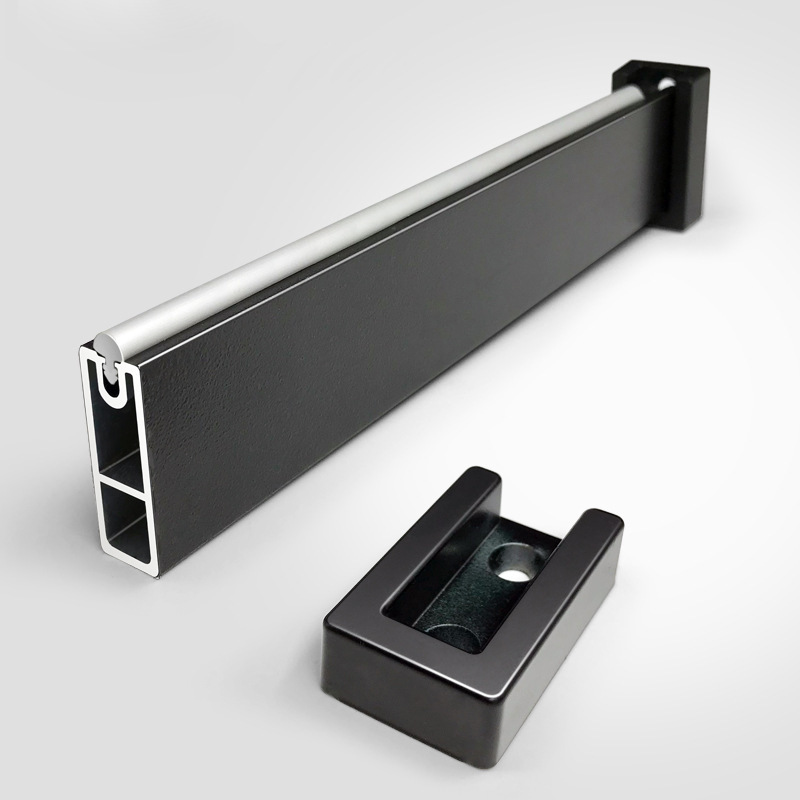
Structural thick-walled extruded profile closet crossbar with precision end-mounting brackets for luxury custom wardrobe systems.
📋 Architectural Guide: Technical Specification of Modern Edge Pull Handles
As the architecture and interior joinery industries gravitate toward unbroken planes and monolithic frontages, edge pull handles (often referred to as tab pulls, profile lips, or top-mount recessed grips) have emerged as the primary alternative to both conspicuous surface-mounted handles and volatile mechanical push-latches. Achieving an optimal balance between mechanical leverage and architectural invisibility requires evaluating three foundational metallurgical and dimensional parameters:
Extrusion vs. Die Casting
Continuous extruded 6063-T5 aluminum alloy offers uniform wall thicknesses (1.2mm–2.0mm) allowing extended lengths up to 3000mm. Conversely, die-cast zinc alloys excel in sculpted organic contours and solid tactile mass for smaller standard-pitch pulls.
Panel Clearance & Kerf Prep
Rear-mounted edge pulls require a minimum door-to-carcass rebate or gap clearance of 2.5mm to 3.5mm. Recessed mortise variations require CNC-milled routed kerfs, ensuring a completely flush rear aesthetic.
Anodization & Micro-Coating
Export-grade finishes demand Class I architectural anodizing (≥15μm) or electrostatically applied fluorocarbon powder coatings to withstand continuous human finger acid, moisture, and alkaline detergents.
For custom cabinet manufacturing, integrating continuous edge profile runs rather than isolated hardware units standardizes shop-floor routing protocols while significantly reducing hardware cycle assembly times.
📈 Global Procurement Trends: The Next Horizon in Architectural Cabinetry Hardware
Sourcing directors, procurement heads, and contract millwork suppliers are navigating a shifting landscape characterized by supply chain consolidation, rising raw material dynamics, and elevated commercial interior specifications. To maintain competitive advantage, international buyers must align their procurement cycles with the following industry developments:
- Consolidated Container Optimization (Mixed Category Loads): B2B importers are shifting away from single-product container shipments. By consolidating aluminum edge profiles, hydraulic concealed hinges, soft-close drawer slides, and wardrobe hanging hardware into unified 40ft HQ shipments directly from a verified Chinese manufacturing hub, buyers trim handling costs by up to 28% and mitigate landed stock imbalance.
- Full-Height Continuous Extrusion Profiles: The demand for modular 100mm–200mm individual edge grips is steadily yielding to full-length continuous vertical edge profiles that run the entire 2400mm–2700mm height of custom wardrobe panels. These extrusions double as anti-warping structural stiffeners for MDF and lightweight honeycomb panels.
- Stringent Surface Durability & Salt Spray Testing: Discerning buyers in Western Europe and North America now mandate documented ASTM-B117 neutral salt spray test results exceeding 96 to 120 hours, ensuring matte black, champagne bronze, and brushed gold finishes resist pitting in humid coastal installations.
- Integrated LED Diffuser Channels: Modern edge pull designs increasingly incorporate co-extruded acrylic light diffusers within the underside grip, marrying tactile ergonomics with ambient architectural illumination in kitchen islands and wardrobe closets.
🔬 Manufacturing Evolution: Precision Metallurgy & Finishing Tolerances
The manufacturing architecture of edge pulls and cabinet fittings has transformed from labor-intensive manual bending to automated, continuous multi-axis CNC machining centers. At Xiamen Vock Hardware, raw aluminum ingots undergo specialized multi-stage processing designed to eliminate visual defects and mechanical failures:
Extrusion Homogenization
Billet heating and automated hot-shear extrusion prevent internal voids, ensuring high tensile strength across the cantilevered grip lip under heavy drawer pull pressures.
CNC Chamfering & Deburring
Computerized multi-spindle end cutting eliminates micro-burrs along the exposed user contact edge, delivering a soft-touch, safe radius (≥0.5mm) on cut profile ends.
Electrochemical Surface Passivation
Automated multi-stage pre-treatment, etching, and sealed anodizing guarantee batch-to-batch color match within Delta E < 0.8 across distinct production runs.
Why Sourcing Professionals Partner with Xiamen Vock Hardware
Rooted in China's prime manufacturing corridor, Xiamen Vock Hardware Co., Ltd. stands as an onsite-verified industrial manufacturer committed to the rigorous requirements of international importers, architectural joinery producers, and commercial project contractors. Backed by an engineering team boasting over 25 years of hardware manufacturing and engineering-order experience, Vock provides the manufacturing resilience required to support continuous, large-scale supply chains.
Rapid Technical Feedback (≤1h)
Supported by a recorded 99.86% response rate, our application engineers address CAD drawings, finish custom requests, and cross-section verifications within 60 minutes.
Low MOQ & Flexible Sampling
We break traditional manufacturing barriers with sample MOQs from 2 pieces on stock lines and low customized production thresholds, facilitating frictionless prototype testing.
OEM, ODM & Buyer Labeling
Full-spectrum custom mold development, private-label laser etching, custom barcoding, and retail-ready drop-tested packaging engineered for wholesale brand elevation.
Frequently Asked Questions by Industrial Importers
What clearance is required between the door and cabinet top when mounting edge pulls?
For standard top-mounted or rear-screwed edge pulls, a minimum gap of 2.5mm to 3.0mm is required between the top door edge and the underside of the countertop or adjacent drawer carcass. If back-beveling or flush mortising is conducted into the door stile via CNC routing, this gap can be minimized to 1.5mm while maintaining unrestricted fingertip leverage.
Can custom lengths, hole-pitch centers, and extruded finishes be fabricated on an OEM basis?
Yes. As an onsite-verified manufacturer, Xiamen Vock Hardware provides comprehensive OEM/ODM engineering. We manufacture custom lengths from 50mm up to 3000mm, machine custom mounting hole spacing, and provide surface finishes including matte black anodized, champagne gold, brushed brass, gunmetal gray, and custom RAL powder coatings matched to your master swatches.
How does Vock Hardware guarantee batch-to-batch color consistency for anodized aluminum hardware?
We deploy closed-loop computer-regulated anodizing tanks where temperature, acid concentration, dye saturation, and immersion timing are digitally controlled. Finished extrusions undergo photometric spectrophotometer testing ensuring that the overall chromatic difference between disparate extrusion runs remains tightly controlled under Delta E < 0.8.
What is your typical lead time and minimum order quantity (MOQ) for production?
For stock models and standardized profiles, our MOQ begins at 10 to 100 pieces, with functional sampling available from 2 pieces. For custom tooling and proprietary extruded profile sections, standard production runs are typically 500 to 1,000 units with an average tooling turnaround of 12-15 days and mass extrusion dispatch within 20-25 days.
Can we consolidate edge pull orders with concealed hinges and drawer slides in one container?
Yes, mixed-category container consolidation is one of our primary core advantages. Clients frequently bundle extruded edge handles, 35mm soft-close hydraulic hinges, undermount slides, wardrobe rods, and kitchen storage baskets into a unified container, eliminating disparate port fees and streamlining customs brokerage.
Upgrade Your Architectural Hardware Sourcing
Connect with the engineering specialists at Xiamen Vock Hardware. Download our complete wholesale technical catalog, structural extrusion specifications, and FOB price sheets today.
Get Catalog